Skip Navigation
Case Studies

PEANUT BUTTER PERFECTION IN EVERY JAR
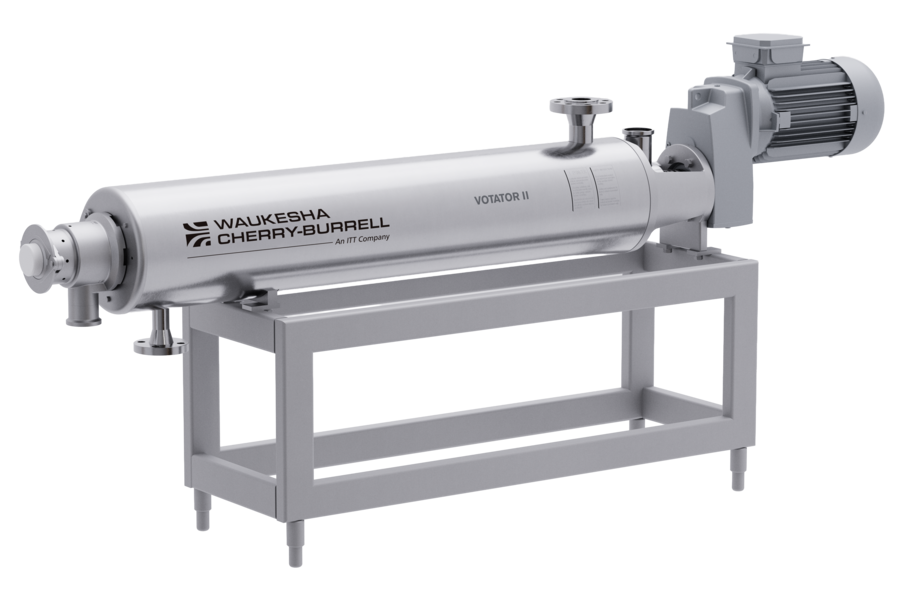
Votator® II Scraped Surface Heat Exchanger

Ruparel Foods Pvt. Ltd., India’s largest private-label peanut butter manufacturer, has become a global leader by combining local sourcing with world-class processing technology. The company supplies major private-label brands worldwide, trusting Ruparel for quality and freshness.Founded in 2007 in Mahuva, Gujarat—India’s peanut heartland—Ruparel Foods has rapidly grown into a world-renowned producer of peanut butter. Its dedication to innovation and quality has earned repeated recognition as the Best Exporter of Peanut Butter from India by IOPEPC (The Indian Oilseeds and Produce Export Promotion Council). Today, Ruparel exports to more than 25 countries across North America, Europe and Asia-Pacific, offering over a dozen varieties—ranging from traditional Crunchy and Natural to inventive flavors like Banana, Chilli, Cinnamon, Coconut and Chocolate.

Solution

The peanut butter finishing solution combines two complementary Waukesha Cherry-Burrell technologies: the Votator II Scraped Surface Heat Exchanger and the Universal 1 ECP pump.

The Votator II uses eccentric scraper blade rotation to continuously renew the heat-transfer surface as peanut butter passes through the unit. This scraped-surface action helps:

  • Improve heat transfer
  • Minimize product buildup on heat-transfer surfaces
  • Provide more uniform cooling
  • Maintain repeatable product exit temperatures
  • Support longer continuous production runs

Precise exit-temperature control is particularly important because it helps stabilize the peanut butter before packaging, reducing the potential for oil separation during storage.

The Votator II is paired with a Waukesha Cherry-Burrell Universal 1 pump, which provides smooth, predictable volumetric flow for viscous products such as peanut butter. Different pump sizes can be selected for individual duties, with one pump providing stable feed into the finishing stage and another transferring finished product toward packaging based on the line configuration and required capacity.

Together, the technologies help maintain consistent residence time, temperature control and gentle product handling throughout the finishing process.

Challenge

The rise of peanut butter manufacturing in India began in the mid-2000s,largely fueled by export demand. From the very beginning, Ruparel Foods recognized a major challenge all peanut butter processors face—oil separation during production. Without precise control of exit temperature, texture and shelf life can quickly suffer. Determined to avoid this issue and make one of the best peanut butters in the world, Ruparel set out to find the ideal combination of ingredients, equipment and processes.As global demand surged, Ruparel also needed a solution capable of scaling production—reliably processing up to 100 metric tonnes per day—while minimizing downtime and maintenance.

Solution

Ruparel understood that making world-class peanut butter required more than just premium ingredients—it required the right technology. Determined to find the best solution, the company launched a global search for advanced processing equipment and traveled to the U.S.to identify the ideal heat exchanger. During this search, they visited a leading U.S. peanut butter manufacturer and discovered the Waukesha® Cherry-Burrell Votator® in action. The superior quality and consistency achieved with this equipment confirmed they had found the right solution.

Ruparel understood that making world-class peanut butter required more than just premium ingredients—it required the right technology.Determined to find the best solution, the company launched a global search for advanced processing equipment and traveled to the U.S.to identify the ideal heat exchanger. During this search, they visited a leading U.S. peanut butter manufacturer and discovered the Waukesha® Cherry-Burrell Votator® in action. The superior quality and consistency achieved with this equipment confirmed they had found the right solution.

Result

  • Enhanced Stability: Precise temperature control minimized oil separation, improving texture and shelf life
  • Efficient Scalability: Consistently processes up to 100 metric tonnes per day, enabling reliable production growth.
  • Trusted Partnership: Ruparel credits Ameya’s technical expertise and support at every stage of its expansion.
  • Market Leadership: Advanced processing technology has positioned Ruparel as a benchmark in Indian peanut butter manufacturing.

Ruparel Foods’ story shows how the right technology can transform a local producer into a global market leader. By adopting the Waukesha Cherry Burrell Votator II and Waukesha Cherry-Burrell PD pumps, the company not only solved critical processing challenges but also unlocked new levels of product quality, consistency and efficiency. Today, Ruparel continues to expand its portfolio, enter new markets and set higher standards for excellence in peanut butter manufacturing.

Learn more about the Votator II Scraped Surface Heat Exchanger

Download PDF

Let's Solve It Together